How to Choose a Profile Bending Machine: 2, 3 or 4 Rollers
How to Choose a Profile Bending Machine: 2, 3 or 4 Rollers
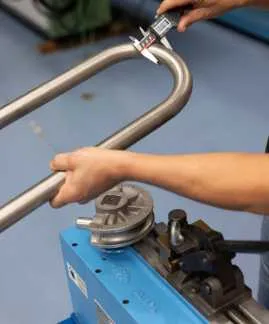
To choose a profile bending machine, start from your part, not the machine: the profile’s type and section, the minimum radius you need, the material and the production volume determine whether a 2, 3 or 4-roll bending machine suits you best. As a general rule, two rollers for simple, low-cost work, three rollers for the most versatile use, and four rollers when you’re after precision, repeatability and minimal waste. Below we break it down so you get it right the first time.
At Curvaser we advise on this purchase every day, and we always start from the same idea: the best bending machine isn’t the one that does the most, but the one that best fits what you actually manufacture. Let’s go step by step.
A quick reminder of how roller bending works
All these machines share the same principle: the profile passes between rollers that pull it through and progressively deform it until it reaches the desired radius. What changes between them is how many rollers are driven and how the work of gripping and bending is split. If you want the full detail of the process, we explain it in our article on what a three-roll bending machine is and how it works.
Two-roll bending machine
On two-roll machines, the material is formed between a drive roller and a counter-roller or bushing. These machines are designed for bending light profile and thin-walled tube at a fixed radius, and are very common for producing rings and simple, repeated shapes.
Their advantage is simplicity and price, plus fast bending on suitable parts. Their limit is a lack of flexibility: changing radius usually means changing tooling, and they’re not the option for heavy profiles or a wide variety of jobs.
Three-roll bending machine
This is the most widespread and versatile configuration. Two rollers drive the material and the third imposes the curve, usually with hydraulic or CNC adjustment. It covers most of a workshop’s needs: it changes radius without specific dies, works a wide variety of sections and delivers a good finish quality.
Its only drawback compared with the four-roll type is that, since it doesn’t properly pre-bend both ends, it leaves straight sections that have to be scrapped. In most cases, that’s an acceptable trade-off for its versatility and price.
Four-roll bending machine
Adds a fourth roller that grips and pre-bends the material from the start. This brings two decisive advantages in demanding production: it minimizes dead ends, making use of almost the entire profile, and it improves repeatability because the material is guided at all times.
It’s the choice for long runs, high-value parts, or when the material savings justify the investment. In return, it’s the most expensive option and requires the most space and maintenance.
Comparison at a glance
|
Criterion |
2 rollers |
3 rollers |
4 rollers |
|
Radius versatility |
Low (fixed radius) |
High |
High |
|
End waste |
Variable |
Noticeable |
Minimal |
|
Repeatability |
Good on fixed parts |
Good |
Excellent |
|
Range of sections |
Limited |
Wide |
Wide |
|
Investment |
Low |
Medium |
High |
|
Ideal use |
Repeated rings and simple shapes |
Versatile workshop |
Long runs and high value |
The criteria that really decide it
Beyond the number of rollers, these are the factors worth putting on the table before requesting a quote:
Profile type and section. Bending thin round tube isn’t the same as bending heavy UPN channel or edgewise flat bar. The maximum section you’ll be working sets the machine’s size and power, and determines the roller set you’ll need.
Minimum radius. The tighter the radius relative to the profile’s size, the more demanding the bend. If you need very tight radii without deforming the section, roller bending may not be the right process — mandrel bending might be.
Material. Steel, stainless steel, aluminium, copper or brass all behave differently under bending. The material affects the torque required, the elastic recovery and the risk of surface marks.
Volume and repeatability. For one-off parts or short runs, a well-adjusted hydraulic machine is enough. For repeated production and tight deadlines, CNC control saves setup time and guarantees part number one thousand is identical to the first.
Material utilization. If you work expensive profiles or large quantities, dead ends translate directly into money. That’s where the four-roll machine’s pre-bending starts to pay off the price difference.
Tooling and service. A bending machine is only as good as its roller set and the support behind it. Make sure you can get tooling for your sections and have technical service and spare parts nearby.
Common buying mistakes
There are three mistakes we see often and that are worth avoiding. The first is choosing the machine based on the catalog’s maximum section without checking the actual minimum radius for that section, which is always more limited. The second is forgetting about tooling and discovering too late that the rollers for your specific profile involve a significant cost or lead time. The third is buying more machine than you need, paying for CNC control or tonnage capacity that the actual job never uses.
New or used?
A profile bending machine has a long service life, so the reconditioned used-machinery market is a reasonable alternative when budget is tight or volume doesn’t justify a new unit. The key is buying from someone who inspects, guarantees and services the machine. We cover this in more detail in our article on new versus used machinery.
When to Recondition Your Machinery and When to Invest in New
CNC or hydraulic: how to decide on control
Beyond the number of rollers, the type of control is the other major decision. A hydraulic bending machine with an on-screen degree readout is rugged, easy to operate and enough for varied work or one-off parts, where the operator adjusts each bend. A CNC bending machine programs the entire cycle (positions, passes and speed) and repeats the part identically regardless of who’s operating it.
The useful question isn’t which is better, but how much you repeat. If you manufacture runs and need unit one thousand to match the first, CNC pays for itself in the setup time it saves. If your work is custom and constantly changing, a good hydraulic machine gives you more machine for less money.
Checklist for talking to your supplier
Come to the conversation with this information ready: you’ll make a better purchase and get a more accurate recommendation.
- Profile type and maximum section you’ll be bending (with dimensions and thickness).
- Usual material or materials (steel, stainless steel, aluminium…).
- Minimum radius you need for that section, not just the maximum section.
- Number of parts and whether they’re repeated or one-off jobs.
- Whether you need to bend in a single plane or more complex shapes.
- Which roller set is included in the price and how much extras cost.
- Warranty, lead time, training and availability of technical service and spare parts.
What the price usually includes (and doesn’t)
It’s worth clarifying from the start what’s included in the quote. The machine’s base price doesn’t always include the full roller set for all your sections, nor training, nor commissioning. These items can make up a significant part of the investment, so ask for them itemized. An offer that looks cheaper can end up costing more once you add the tooling you’ll actually need.
Don’t forget space and installation
A profile bending machine takes up space and needs certain minimum conditions: a clear area for handling long bars, an electrical supply matched to its power, and, on larger machines, an adequate foundation. Before closing the purchase, check that the machine fits your workflow, not just your workshop. Thinking through the logistics of material in and out avoids surprises on installation day.
A purchase that looks to the future
Choose with the coming years in mind, not just today’s order. If you expect to grow or diversify the sections you work, leaving some capacity headroom and making sure tooling is available for more profiles can save you a second purchase in the near term. Balancing today’s investment with tomorrow’s flexibility is, in the end, what sets a good decision apart.
Frequently asked questions
How many rollers do I need if I only bend simple, repeated rings?
For producing rings of a fixed section, a two-roll bending machine may be the fastest, most affordable option. If you want radius flexibility, step up to three rollers.
Is a four-roll machine worth it for a small workshop?
Only if you work expensive profiles or long runs where the material savings from pre-bending offset the higher investment. For a versatile workshop, the three-roll machine is usually the ideal balance.
Does a used machine give good results?
Yes, if it’s inspected and guaranteed by a supplier with technical service. It’s a sensible way to get started or expand capacity without the outlay of a new unit.